Problem
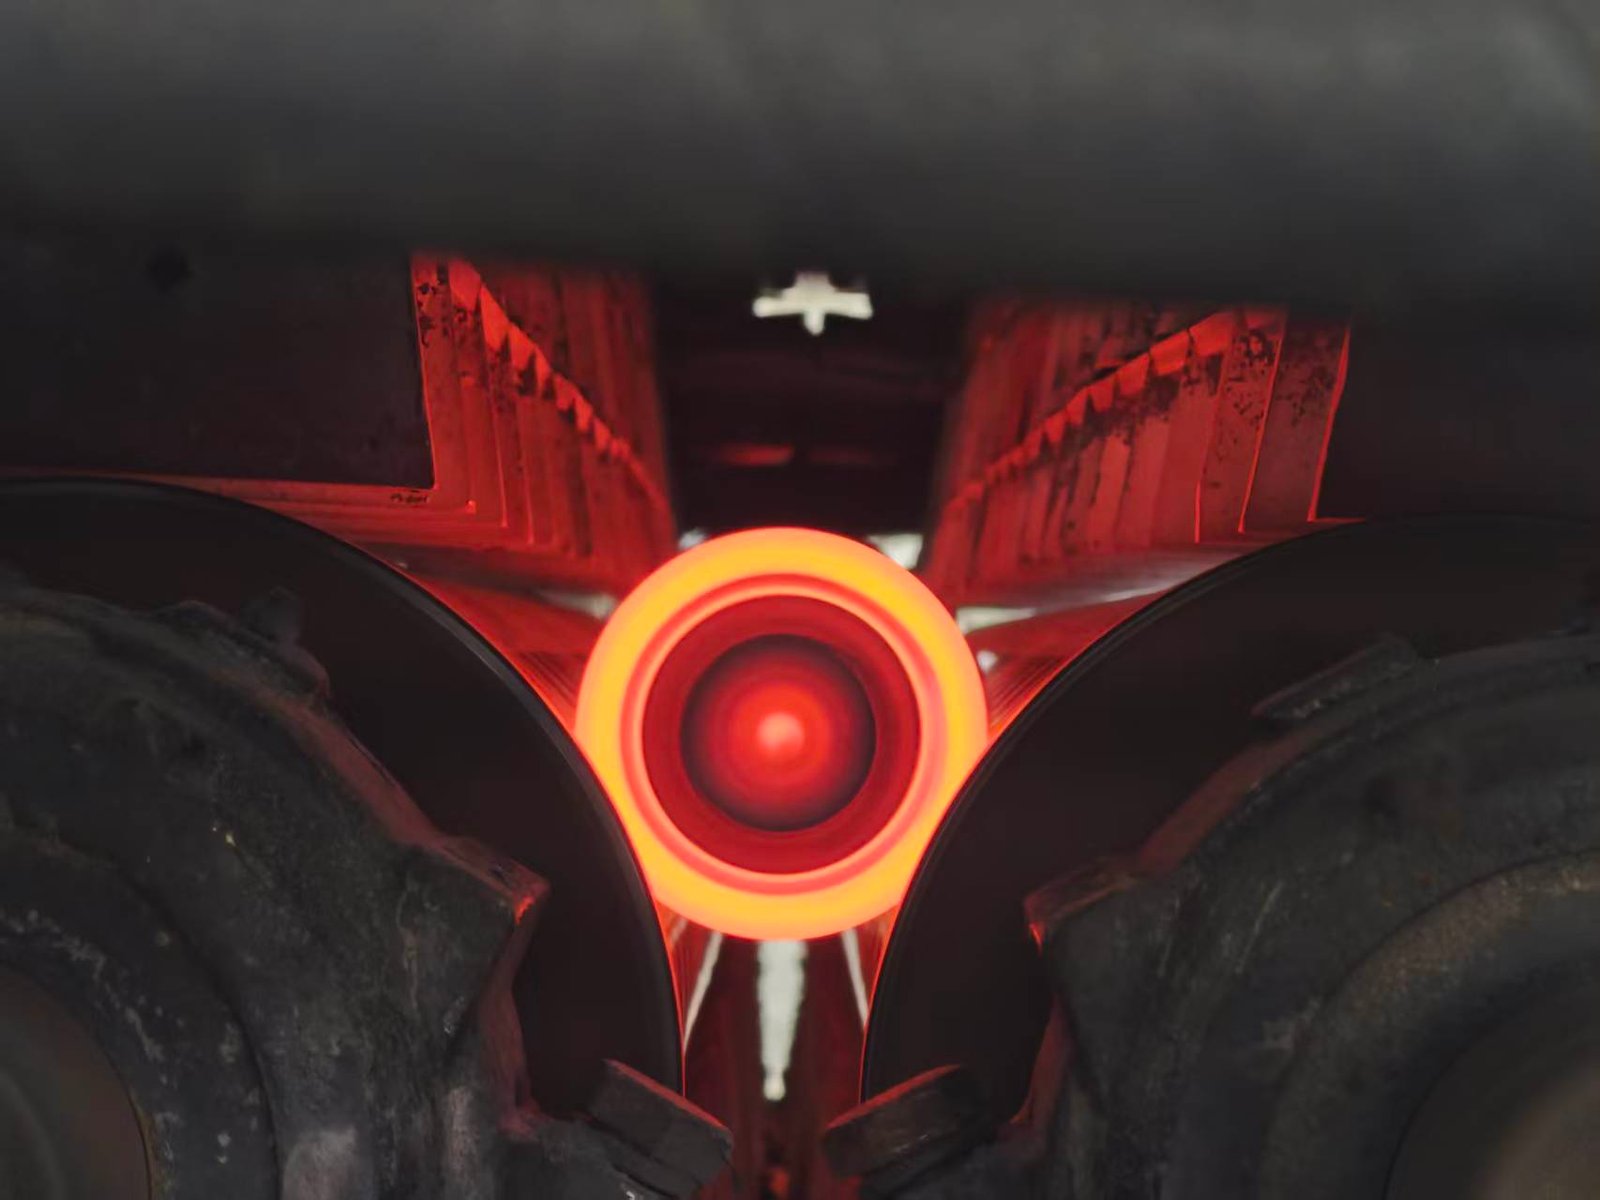
Foreign particles, unmelted pellets or degraded material clog the screw, check ring or nozzle, causing pressure spikes, short shots and unplanned cleaning downtime.
Typical Causes
- 01Regrind and recycled streams carrying metal, paper or incompatible debris.
- 02Unmelted pellets from inadequate screw geometry or low L/D.
- 03Degraded, charred material building up in dead zones and stagnation areas.
- 04Worn screw flights creating dead zones where material accumulates.
- 05Inadequate screening before the nozzle or hot runner.
Technical Challenges
- Preventing blockage without restricting flow.
- Maintaining melt quality and consistency.
- Avoiding cross-contamination between material changes.
- Reducing cleaning and purging downtime.
Rootier's Technical Solutions
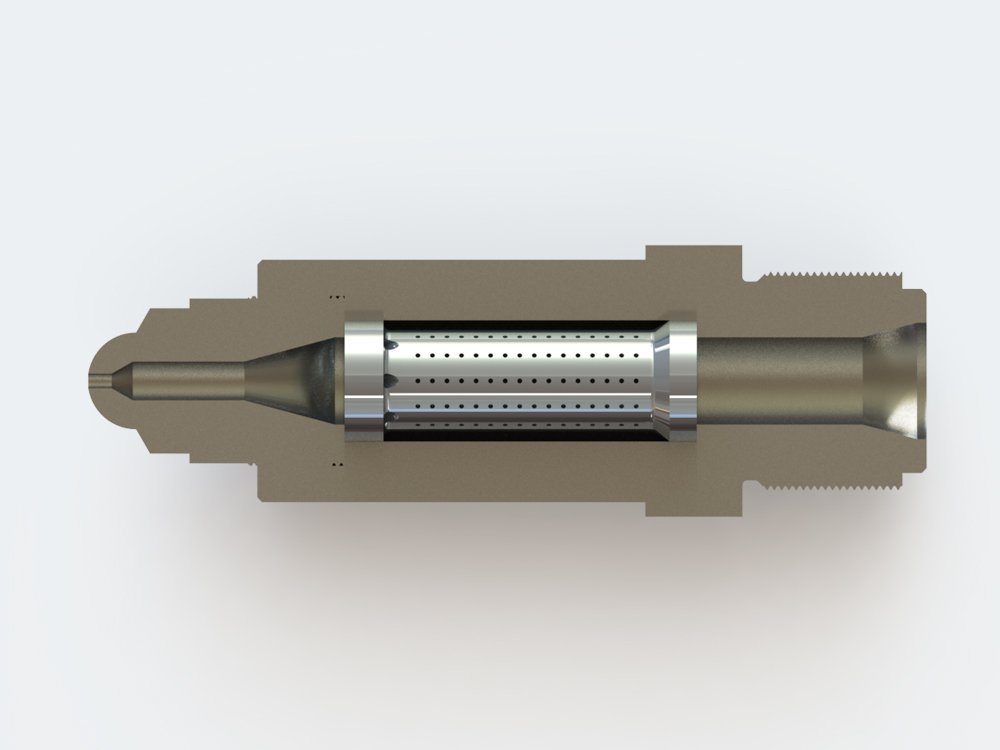
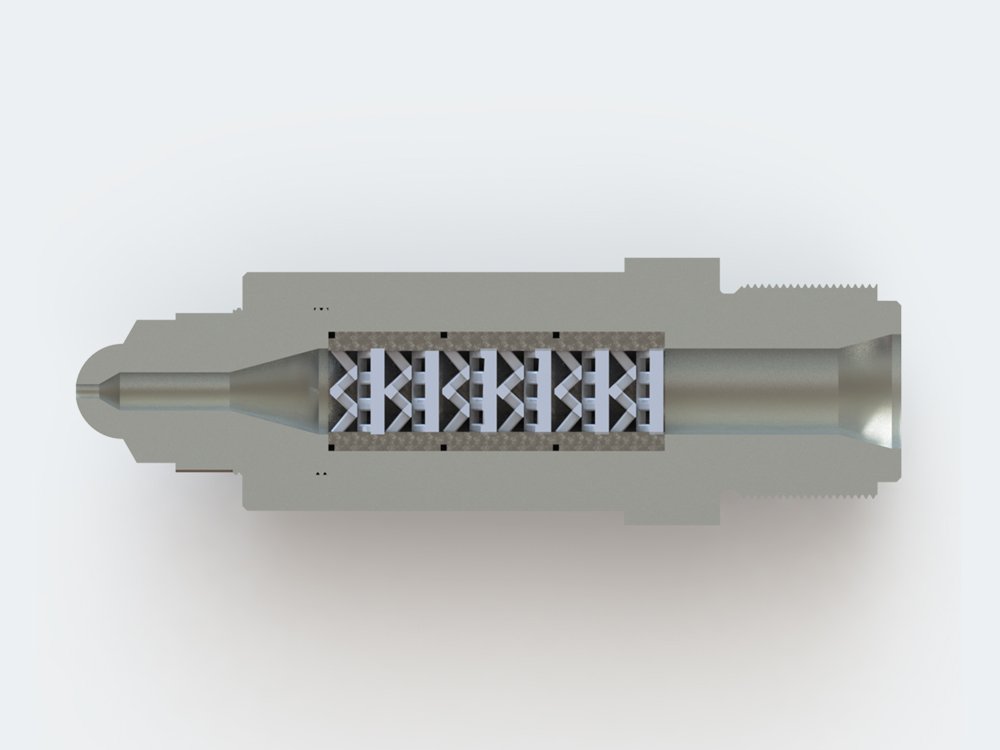
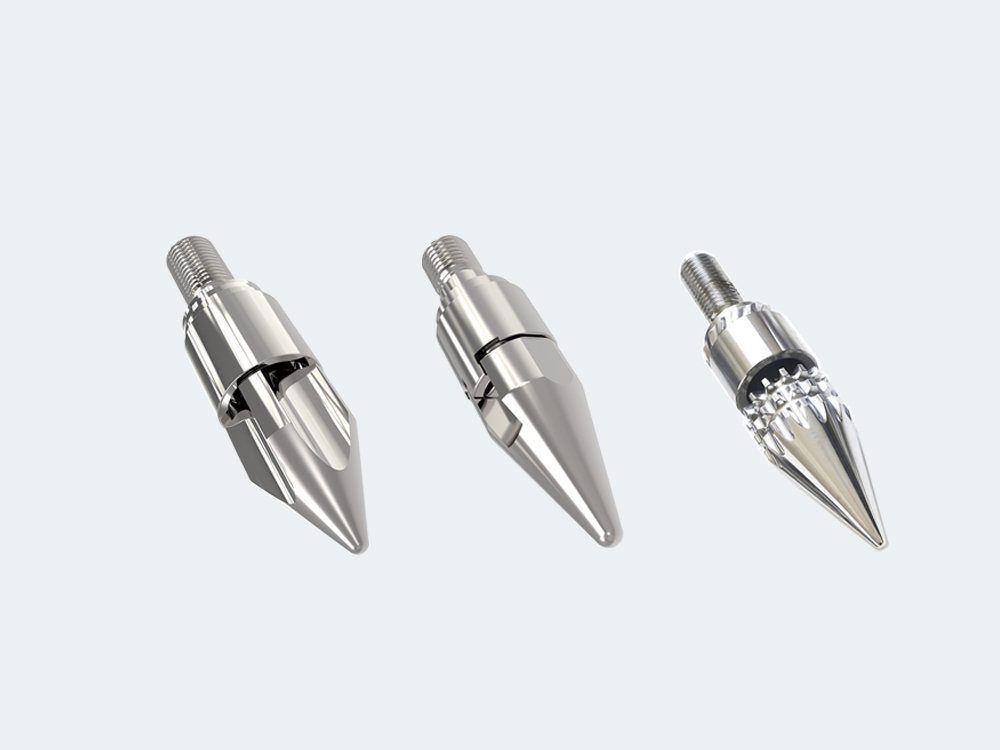
- 01Filter nozzles that screen foreign particles before the mould.
- 02Optimised screw geometry with no dead zones for complete melting.
- 03Bimetallic barrels that resist wear and keep bore smooth.
- 04Electropolished / mirror surface treatments that reduce material adhesion.
- 05Material-handling and purging guidance to limit contamination.
Recommended Products
Applications / Materials
Recycled and regrind processingCompounding and masterbatch linesFood-grade and medical productionFrequent material-change operations
Frequently Asked Questions
A filter nozzle screens foreign particles before the mould, while an optimised screw geometry with no dead zones ensures complete melting. Smooth surface treatments reduce material buildup.
Regrind streams can carry metal, paper or incompatible debris, and uneven flake size causes unmelted pellets. A filter nozzle and bimetallic barrel help maintain melt quality on recycled material.
Yes. ROOTIER manufactures filter nozzles to your machine connection and processing requirements, with appropriate screen mesh for the resin and contamination risk.